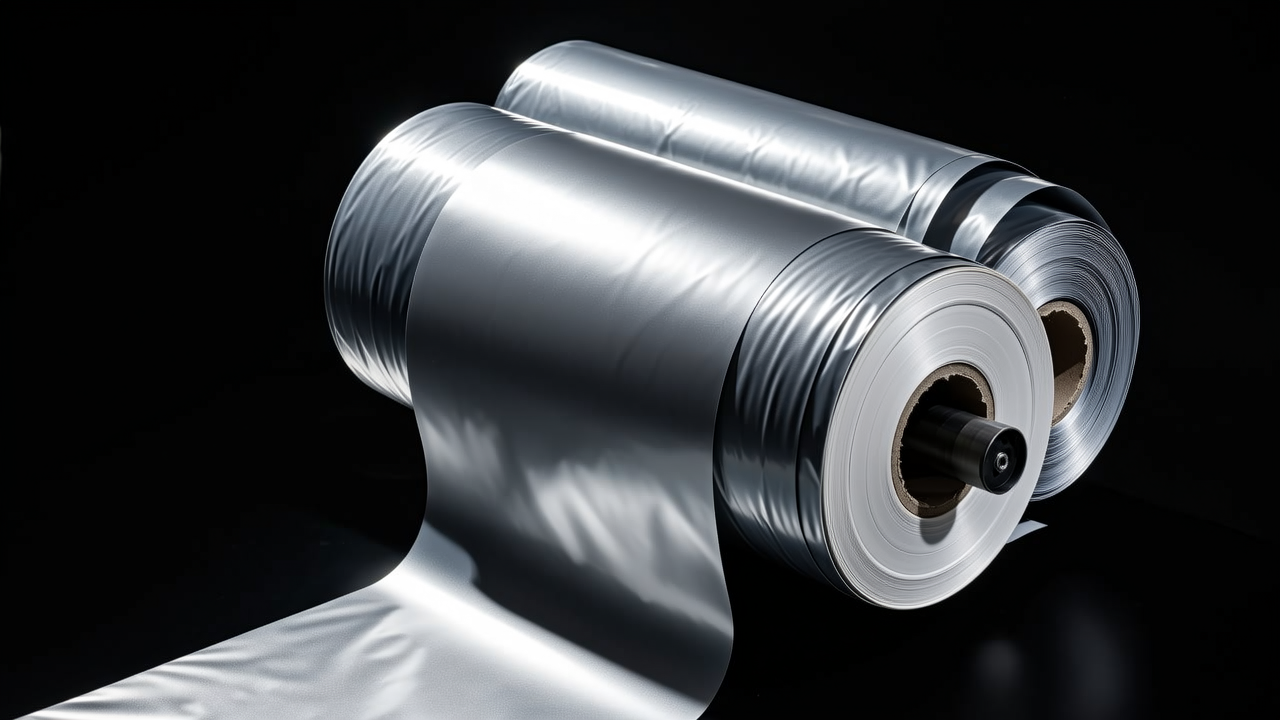
Of the ways to bond layers in flexible packaging, extrusion lamination is the one built for volume. Instead of coating and drying an adhesive first, it melts resin and extrudes it as a thin film that bonds two substrates together while still hot. For large, stable orders in food and household products, that usually makes it the most economical route. Here is how it works, where it fits, and what to control on the line.
Extrusion Lamination vs Dry Lamination
Dry lamination applies an adhesive to a substrate, dries off the solvent, and then presses a second layer on. Extrusion lamination melts LDPE, EAA or EVA in an extruder and pushes it through a T-die as a thin molten curtain, which is nipped between two substrates and cooled into a single structure.
The essential difference is where the bonding layer comes from: a pre-applied adhesive versus resin extruded on the spot. That single choice drives cost structure, environmental profile and the batch sizes each method suits.
The Extrusion Lamination Process
A typical line runs through five stages.
Unwind and tension control. Both substrates unwind under steady tension; variation here shows up later as wrinkles and curl.
Corona or primer treatment. Extruded resin does not always grip every substrate well, so a corona discharge or a thin primer is applied to raise bond strength.
Extrusion casting. Resin is melted, filtered and pushed through the die; film thickness and uniformity depend on die gap and chill roll speed.
Nipping and cooling. The molten film meets both substrates at the nip roll and is then set on chill rolls.
Rewind and curing. The roll cures for a set period so bond strength stabilises before slitting or pouch making.
Why High-Volume Production Prefers It
Lower cost. No adhesive and no drying tunnel means fewer consumables and better material utilisation. The gap widens as order volume grows.
Higher speed. Line speeds are high and continuous, which suits long runs and makes lead times more predictable.
Cleaner process. There is no solvent-based adhesive, so solvent residue and VOC emissions from drying are largely removed. That eases both workplace air quality and regulatory exposure.
Flexible structure. One extrusion pass can bond and thicken at the same time; changing the resin grade adjusts heat-seal behaviour and flexibility without redesigning the whole structure.
Concept packaging visual generated for editorial use. Not a customer project, not a tested structure.
Common Structures and Material Pairings
The classic build is print film, extruded resin, sealant film. BOPP or PET carries print and strength on the outside, LDPE is extruded as the bonding and bulking layer, and CPP, LDPE or EVA provides a low-temperature seal on the inside. Where more barrier is needed, foil or metallised film is kept in the structure and the extrusion layer ties it together.
A simple rule keeps selection sane: barrier comes from the substrates, bonding and sealing come from the extruded layer.
Limits and Quality Control
Extrusion lamination is not universal. Bond strength is generally lower than a good dry-lamination structure, so it may fall short for retort or chemically aggressive products, and extrusion thickness uniformity and gel control depend heavily on equipment precision.
Four checkpoints matter most. First, peel strength, sampled per batch at both the edge and the centre of the web. Second, thickness uniformity, because large cross-web variation makes heat sealing unstable. Third, gels and odour, since unmelted resin and contamination show up in appearance and smell. Fourth, curing time and tension management, which decide whether the finished roll curls or delaminates.
If a product needs high barrier, retort performance at 121 C, or small and frequently changing volumes, dry lamination is often the better fit. For long, stable runs, extrusion lamination is hard to beat on cost.
Choosing Between the Two
Recent work on mono-material PP for retort applications shows how closely bonding choices and material selection are tied together.
Selecting a lamination method is really a balance between volume, cost, environmental targets and performance. Extrusion lamination earns its place through scale efficiency: it extrudes the bonding layer directly and trades a little bond strength for lower cost, faster throughput and a cleaner line. If you are weighing up which route suits your product, contact OMOpack and we will work through the structure with your volumes and end use in mind. You can also browse the wider selection of flexible packaging structures at OMOpack.com.
Water vapour transmission rate is measured by ASTM F1249, the method most specifications quote alongside oxygen data; food-contact assessment for the EU market is summarised on EFSA’s food contact materials topic page.
Conclusion
Extrusion lamination is a volume decision more than a quality decision. Where orders are long and the structure is stable, extruding the bonding layer buys lower cost, higher line speed and a cleaner process, at the price of some bond strength. Where the product needs retort performance, high barrier, or where batches are small and change often, dry lamination remains the safer route. Fix the volume and the end use first, then choose the method that fits them.
Frequently Asked Questions
When is extrusion lamination the wrong choice?
When the pack needs high barrier, retort performance at 121 C, or when volumes are small and the structure changes often. Extrusion lamination trades a little bond strength for throughput, cost and a cleaner line, so it is least comfortable where bond strength or heat resistance is the limiting requirement. The first thing to check is the contents and the sterilisation route: if the product has to survive retort or aggressive contents, look at dry lamination before comparing prices.
How is bond strength checked before a batch is released?
By testing peel strength per batch, with samples taken from both the edge and the centre of the web. Centre and edge behave differently because extruded film thickness varies across the width, and that variation is what eventually shows up as poor seals or delamination in the field. Gels, unmelted resin and odour are checked on the same sample, because they point to the same underlying problem: extrusion conditions that were not stable across the run.
Does extrusion lamination eliminate solvent emissions?
It removes the drying step, which is where most solvent emissions come from in dry lamination, because there is no solvent-based adhesive to dry off. That cuts solvent residue and VOC emissions from the line, and eases workplace air quality and regulatory exposure. It does not make the process emission-free: the extruder still melts resin and produces heat and odour, and resin handling has its own requirements. The meaningful comparison is extrusion against dry lamination on the same product, not extrusion against zero.
What goes wrong if the curing time is cut short?
The roll moves to slitting before bond strength has stabilised, and the failure appears later as curl, tunnelling or layer separation. Curing is not padding in the schedule; it is part of the bond formation, and shortening it to gain a day usually costs more than the day is worth. Tension management belongs to the same checkpoint, because a roll wound too tightly will curl even when the cure has been given its full time.